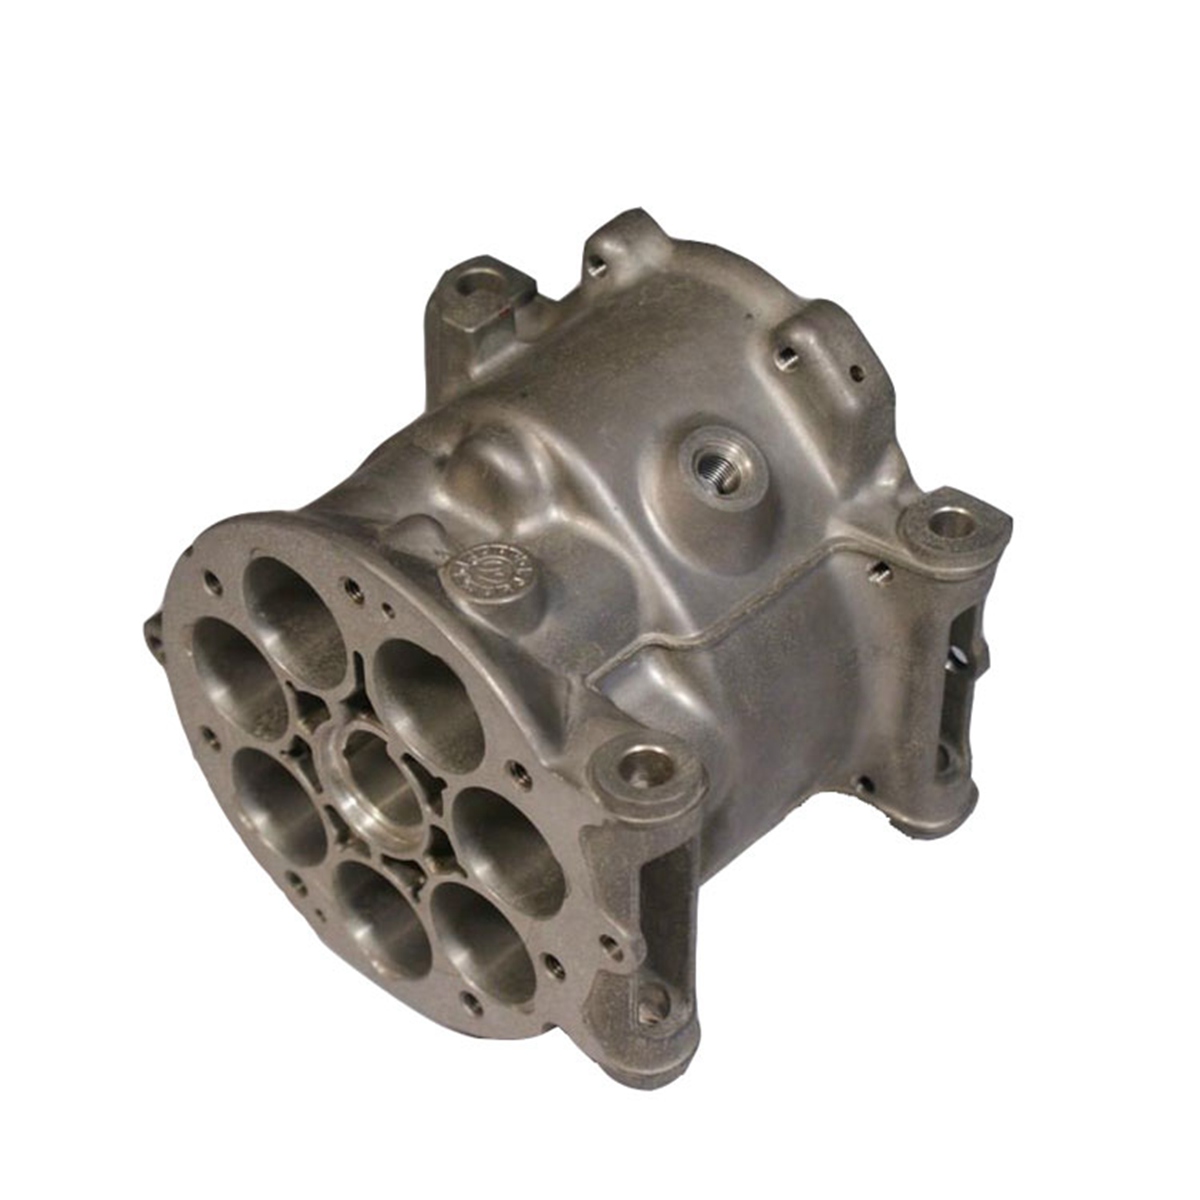
Investment casting tooling costs can vary significantly from one project to another. Some tooling may cost only a few hundred dollars, while others require several thousand dollars or more. The difference is not determined by a single factor but by the combination of part design, tooling requirements, manufacturing complexity, and expected production volume.
Understanding what drives investment casting tooling costs allows buyers to make informed design decisions before tooling is manufactured. In many cases, small design adjustments made early in the development stage can reduce tooling costs without affecting the performance of the final casting.
Part Size
The overall size of the casting is one of the most direct factors affecting investment casting tooling costs.
Larger components require larger tooling blocks, more machining time, and additional material to manufacture the mold. Large tooling may also require specialized machining equipment and handling during production, increasing the overall tooling investment.
In general, larger castings require:
More tooling material
Longer CNC machining time
Higher manufacturing costs
Increased maintenance requirements
As a result, tooling costs usually increase as part size increases.
Part Complexity
Complex part geometry is another major contributor to investment casting tooling costs.
Features such as thin walls, deep cavities, sharp corners, undercuts, and intricate internal structures make tooling more difficult to manufacture. These features may require additional inserts, sliders, or special machining operations, increasing both design time and manufacturing costs.
Design characteristics that commonly increase tooling costs include:
Thin wall sections
Undercuts
Deep recesses
Complex internal cavities
Multiple intersecting features
Tight radii
Whenever possible, simplifying the product design can reduce tooling complexity and lower overall costs.
Tool Material
The material used to manufacture the tooling also affects investment casting tooling costs.
For lower production volumes, aluminum tooling is often a cost-effective choice because it is easier to machine and has a lower manufacturing cost.
For medium- and high-volume production, hardened steel tooling is commonly selected due to its longer service life and greater resistance to wear.
Although steel tooling has a higher initial cost, it can provide better long-term value for projects requiring large production quantities.
Number of Cavities
The number of cavities built into the tooling directly influences tooling costs.
A single-cavity tool produces one wax pattern per injection cycle and typically has the lowest manufacturing cost.
A multi-cavity tool produces several wax patterns during each cycle, improving production efficiency but requiring a larger and more complex tooling design.
While multi-cavity tooling increases the initial investment, it can significantly reduce production costs for high-volume orders by improving manufacturing efficiency.
Tolerance and Surface Finish Requirements
Products with tight dimensional tolerances or demanding surface finish requirements often require more precise tooling manufacturing.
Additional machining accuracy, polishing, and quality verification increase the time needed to produce the tooling, resulting in higher investment casting tooling costs.
Requirements that commonly increase tooling costs include:
Tight dimensional tolerances
High surface quality
Precision sealing surfaces
Complex mating features
Cosmetic appearance requirements
Before specifying extremely tight tolerances, buyers should evaluate whether they are necessary for the product’s intended function.
Investment casting tooling costs are influenced by many interconnected factors rather than a single design feature. By considering part size, geometry, tooling material, cavity configuration, and quality requirements during the design stage, buyers can better control tooling expenses while maintaining the performance and reliability of the finished casting.